| 1. Select the Rubber Compound According to the Working Environment |
| Material | NBR
Nitrile rubber | Approximately −30°C to +100°C
Some specialized compounds can operate at higher temperatures for limited periods. | Good resistance to mineral oils, hydraulic oils, fuels, and abrasion. | Hydraulic and pneumatic seals, oil systems, general industrial equipment. | Limited resistance to ozone, weathering, sunlight, and many polar solvents. | Request the acrylonitrile content, hardness, temperature rating, and oil-immersion test data. |
| Material | FKM
Fluoroelastomer | Approximately −20°C to +200°C
Compound-specific limits apply. | Strong resistance to fuels, mineral oils, many chemicals, high temperature, and ozone. | Fuel systems, high-temperature machinery, chemical-process equipment, vacuum applications. | Usually unsuitable for hot water or steam, some amines, strong alkalis, and certain low-temperature applications. | Confirm the compound family, low-temperature flexibility, chemical compatibility, and compression-set results. |
| Material | EPDM
Ethylene propylene rubber | Approximately −50°C to +150°C
Steam and hot-water ratings depend on the formulation. | Excellent resistance to hot water, steam, weathering, ozone, and many diluted acids and alkalis. | Water valves, cooling systems, outdoor equipment, brake fluids based on glycol, and steam-related service. | Generally not compatible with petroleum oils, mineral-oil greases, and many hydrocarbon fuels. | Confirm whether the application contains mineral oil or fuel and request hot-water or steam test evidence. |
| Material | VMQ
Silicone rubber | Approximately −60°C to +200°C
Short-term exposure may be higher depending on the compound. | Excellent resistance to temperature extremes, ozone, weathering, and many environmental conditions. | Static seals, food-contact equipment where properly certified, medical devices, and high/low-temperature applications. | Lower tear, abrasion, and tensile strength than many other elastomers; poor resistance to many fuels and oils. | Confirm tensile strength, tear strength, compression set, color requirements, and applicable regulatory certificates. |
| Material | FFKM
Perfluoroelastomer | Often approximately −20°C to +300°C
Actual limits are highly compound-specific. | Very broad chemical resistance and excellent high-temperature performance. | Semiconductor, chemical processing, laboratory, and demanding high-temperature sealing systems. | High material cost; low-temperature flexibility and availability vary by compound. | Request compound-specific chemical compatibility, compression-set data, lead time, and lot traceability. |
| Material | PTFE
Polytetrafluoroethylene | Approximately −200°C to +260°C in many service conditions. | Very broad chemical resistance and low friction. | Static seals, chemical equipment, valve systems, and applications requiring low friction or chemical inertness. | Low elasticity and tendency to creep; installation design and energizing method are important. | Confirm whether the part is a solid PTFE ring, filled PTFE ring, or elastomer-energized seal. |
| 2. Define the O-Ring Size and Geometry |
| Size standard | AS568 inch series | Nominal inside diameter and cross-section are defined by an established inch-based size series. | Commonly used in North American industrial, hydraulic, pneumatic, and aerospace-related designs. | Equipment designed around inch dimensions and replacement parts. | Nominal size does not by itself define material, hardness, tolerance, or application performance. | Provide the dash number or exact inside diameter and cross-section; do not rely only on a visual sample. |
| Size standard | ISO 3601 series | Metric and inch-related O-ring dimensions are covered according to the applicable part of the standard. | Suitable for standardized industrial sealing designs when the correct class and tolerance are selected. | General industrial, hydraulic, and pneumatic equipment. | Different standard classes and application requirements may use different tolerances. | State the standard, size code, application class, and dimensional tolerance required. |
| Size standard | Metric O-ring sizes | Specified by inside diameter and cross-section in millimeters. | Useful for equipment designed with metric grooves and locally available components. | Industrial machinery, pumps, valves, appliances, and custom equipment. | A similar-looking inch size may not provide the correct squeeze or groove fill. | Send measured inside diameter, cross-section, groove dimensions, and a technical drawing. |
| Geometry | Cross-section and inside diameter | Both dimensions affect squeeze, stretch, groove fill, and pressure capability. | Correct geometry supports reliable sealing and reduces extrusion or installation damage. | All static and dynamic O-ring applications. | Measuring a used or deformed O-ring can produce inaccurate dimensions. | Measure an unused part where possible and identify whether dimensions are nominal or actual. |
| Geometry | Groove design | Groove width, depth, corner radius, surface finish, and gland fill must match the O-ring. | Proper gland design helps control leakage, extrusion, friction, and compression set. | Static face seals, radial seals, reciprocating seals, and rotary seals. | An O-ring cannot compensate for an incorrect groove, excessive clearance, sharp edges, or poor surface finish. | Provide a 2D drawing with groove dimensions, mating materials, pressure, and movement type. |
| 3. Specify Performance Requirements |
| Hardness | 70 Shore A | A common general-purpose hardness for many industrial O-rings. | Balances flexibility, sealing contact, and resistance to extrusion in moderate conditions. | General static seals and many low-to-moderate pressure applications. | May not be optimal for very low-temperature sealing, high-pressure extrusion, or delicate installation. | Specify hardness tolerance, test method, and whether the value applies to the finished part or test slab. |
| Hardness | 90 Shore A | Higher hardness can improve extrusion resistance under suitable design conditions. | More resistant to deformation than softer compounds in some high-pressure applications. | High-pressure hydraulic seals and applications with larger extrusion gaps, when properly designed. | More difficult to install and less tolerant of dimensional irregularities or low-temperature contraction. | Confirm pressure, clearance gap, backup-ring requirements, and installation tooling. |
| Pressure | Static sealing | Pressure capability depends on material, hardness, clearance gap, temperature, and groove design. | Generally more tolerant than dynamic sealing because there is little or no relative motion. | Flanges, covers, plugs, end caps, and stationary joints. | High pressure can cause extrusion, nibbling, or permanent deformation if the gland is unsuitable. | Provide maximum and minimum pressure, pressure cycling, clearance gap, and backup-ring requirements. |
| Movement | Dynamic sealing | Reciprocating and rotary applications require material, surface finish, lubrication, and groove design review. | Friction, wear, heat generation, and stick-slip become important performance factors. | Hydraulic cylinders, pneumatic cylinders, rotating shafts, and moving valves. | A compound suitable for static service may wear rapidly in dynamic service. | State speed, stroke or rotation, pressure, lubrication, surface hardness, roughness, and cycle count. |
| Compression set | Low compression set requirement | Important for long-term sealing at elevated temperature or under continuous compression. | Lower compression set generally helps the seal retain contact force over time. | Flange seals, engine compartments, high-temperature equipment, and long-life assemblies. | Test results depend on temperature, duration, specimen geometry, and test method. | Request the test standard, test temperature, test duration, and measured result. |
| Cleanliness | Low-particle or controlled-cleanliness production | Required when contamination can damage equipment or affect product quality. | Relevant to medical, food, semiconductor, laboratory, hydraulic, and precision applications. | Clean assemblies, fluid-control equipment, and sensitive manufacturing systems. | Ordinary production and packaging may not meet controlled-cleanliness requirements. | Confirm washing process, inspection environment, packaging method, particle limits, and certificates. |
| 4. Evaluate the OEM Factory Before Ordering |
| Technical capability | Tooling and mold control | The factory should control mold dimensions, parting lines, flash, and cavity consistency. | Stable tooling helps maintain cross-section, inside diameter, appearance, and batch repeatability. | Custom sizes, nonstandard profiles, high-volume production, and tight-tolerance parts. | Poor mold maintenance can create flash, dimensional drift, and inconsistent sealing. | Ask for mold-flow or tooling review, cavity control, mold-maintenance records, and sample approval procedures. |
| Quality system | Documented quality control | Incoming material, mixing, molding, trimming, inspection, and final packing should be controlled. | Documented controls improve traceability and reduce variation between production lots. | OEM programs, regulated sectors, export orders, and long-term supply arrangements. | A certificate alone does not prove that the specific compound and process meet the application need. | Request process-control records, inspection plans, calibration records, nonconformance handling, and lot traceability. |
| Material verification | Compound identification and batch traceability | Each production lot should be linked to a controlled material batch and formulation record. | Helps prevent material substitution and supports investigation of field failures. | Critical seals, chemical service, safety-related equipment, and repeat orders. | Generic material names such as “rubber” or “oil-resistant” are not sufficient specifications. | Specify polymer type, hardness, color, cure system if relevant, material certificate, and batch number. |
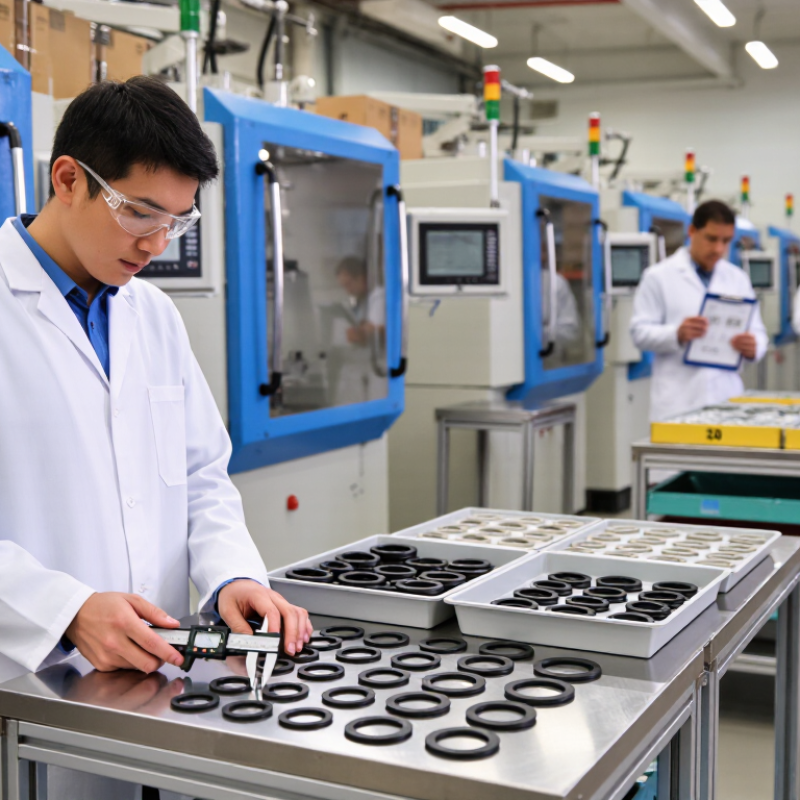
| Inspection | Dimensional and visual inspection | Inspection should cover inside diameter, cross-section, flash, surface defects, and deformation. | Reduces leakage caused by incorrect dimensions, cuts, cracks, voids, or excessive mold flash. | Every application, especially high-volume and safety-critical production. | Sampling alone may not detect every defect unless the sampling plan is defined and appropriate. | Agree on drawing tolerances, acceptance limits, sampling level, inspection tools, and inspection report format. |
| Validation | Application-specific testing | Testing should reproduce the actual temperature, pressure, fluid, movement, and service duration where practical. | Application testing provides more useful evidence than a general material datasheet alone. | New compounds, unusual fluids, high pressure, high temperature, and dynamic service. | Laboratory results may not represent the exact groove, fluid, or operating cycle in the final equipment. | Request a validation plan covering leakage, compression set, immersion, pressure cycling, and dynamic wear as applicable. |
| Commercial reliability | Sampling, production, and delivery control | Reliable supply requires controlled sample approval, repeatable production, packaging, and shipment records. | Helps maintain consistent quality throughout the product life cycle. | Custom OEM parts, scheduled maintenance programs, and recurring production orders. | Low initial price may not reflect tooling, inspection, packaging, or failure-related costs. | Confirm sample lead time, tooling ownership, minimum order quantity, production lead time, packaging, and replacement policy. |
| 5. Minimum Information to Include in an OEM RFQ |
| Required input | Part identification | Part number, drawing revision, sample quantity, and intended annual volume. | Prevents confusion between similar sizes and revisions. | All custom and standard O-ring purchasing projects. | Incomplete identification can result in incorrect tooling or an unsuitable quotation. | Include a drawing, 3D file if needed, sample photos, and clear revision control. |
| Required input | Operating conditions | Temperature range, pressure range, fluid or gas, movement, speed, and cycle frequency. | These conditions determine compound selection and seal design. | Static, reciprocating, rotary, vacuum, hydraulic, pneumatic, and chemical service. | “High temperature” or “chemical resistant” without numerical conditions is ambiguous. | Provide minimum, normal, and maximum operating conditions, including transient peaks. |
| Required input | Quality and compliance | Hardness tolerance, appearance limits, dimensional tolerances, certificates, and testing requirements. | Transforms general expectations into measurable acceptance criteria. | OEM production, regulated industries, export supply, and critical sealing applications. | Requirements added after production may increase cost and delay delivery. | Define inspection standards, documentation, packaging, labeling, and lot-release requirements before quotation. |